
General requirements for cold rolling plant and workshop layout
author: Glimpse
2022-12-07
General requirements for cold rolling plant and workshop layout
This article lists the requirements for considering the cold rolling technology and the workshop layout in the cold rolling design, and must be paid attention to during the design stage. Cold rolling process equipment and workshop layout are very critical to the successful operation of the cold mill plant project in the future.
Keywords: cold rolling engineering , cold rolling plant, workshop layout
According to many years of cold rolling engineering experience, GLIMPSE TECHNOLOGY has summarized the general requirements of cold rolling equipment and workshop layout as follows:
1 Pickling workshop should be arranged separately, or the wall skin is used to separate the pickling workshop from other workshops. The relevant facilities and equipment in the pickling workshop should be taken to prevent acid -proof measures and should be well ventilated.
2 The hot -rolled strip -steel production for cold -rolled carbon steel and the production of cold -rolled silicon steel should be washed by the hydrochloric acid washing process.
3 Various acid liquids, alkali, and electrolyte circulation systems in cold rolling production units should have detection and control functions such as concentration, temperature, and liquid level.
4 Various pickled slots and acid liquid circulation tanks in cold rolling production units, alkaline grooves and alkaline fluid circulation systems, electroplating grooves and electrolyte circulation systems, and subsequent rinsing tanks and rinsing water circulation tanks, and the corresponding area of the corresponding area Pitches, etc., should be set up with a sour or alkali fog ginseng purification system.
5 The hydrochloric acid, nitric acid, and hybrid acid waste liquid composed of nitric acid and hydrofluoric acid during cold rolling production should be resourceful.
6 The racks, rolls and transmission shafts of various cold rolling machines and flat machines should be set up with overload protection devices.
7 Except for hydraulic pressure (pressure above), automatic thickness control (AGC), and oil mist purification system with hydraulic pressure (pressure above), the newly built or rebuilt cold rolling machine should also have the following functions:
1) Direct detection and control;
2) The full-continuous cold rolling machine that produces cold rolled steel, the possibility of the production of cold-rolled carbon steel and cold-rolled silicon steel-rolling machines, and the dynamic change specifications of cold-rolling, annealing, and pickling units of cold-rolled stainless steel It
3) Rolling parameters are preset.
8 Anti -slip measures should be set up in the operation area of cold rolling machines and flat machine.
9 Cold -rolled machine and a separate setting units, which are set up around the work area of the machine, a safety protection device should be set up.
10 cold rolling machines, skin pass mills, and underground oil depots of other production crews should be set up with ventilation systems.
11 Various cold rolled annealing furnaces should have a mild furnace pressure detection and control function. For an antidant furnace that uses restored protection atmosphere, it should also have the detection and control function of hydrogen content and dew points.
12 The water spraying, water fog or invasive water quenching device after the annealing of steel should be set.
13 Various cold rolled annealing furnaces should be recovered and utilized by flue gas heat heat.
14 The cold-rolled induction annealing furnace should be provided with measures to prevent electromagnetic field harm to surrounding equipment and personnel.
15 Cold -rolled annealing furnaces should abide by the following safety regulations:
After the atmosphere and air in the furnace reaches a certain mixing ratio, there is a possible heat treatment furnace at a certain temperature. The explosion -proof device must be set on the corresponding part of the furnace body.
For the atmosphere in the furnace with hydrogen content higher than 5%, the hydrogen should be burned in the heat treatment furnace, or the atmosphere should be discharged out of the factory building through pipelines;
The inlet and outlet of the cooling section of the continuous annealing furnace containing more than 5% hydrogen must be equipped with a sealed isolation device, and equipped with an automatic furnace pressure control, automatic nitrogen purge and discharge system
The combustion device with compulsory air delivery should be provided with a stop device or an automatic partition valve on its gas support.
The gas pipeline and air pipeline of the combustion device should have a low -voltage alarm device;
The end of the air pipeline should be provided with a dispersion tube, and the dispersion tube should be led to the factory of the plant;
The hydrogen pipes that are connected to the hydrogen equipment should be cut off, and the hydrogen equipment with a bright fire should also be provided with a fireproofer.
In the furnace area, the gas platform and operating venue shall be set up in a certain number of fixed carbon monoxide detectors, and the sound and light alarm instructions shall be set up. The operating platform should have a gas alarm terminal display.
16 Cold -rolled annealing stove chimney design must meet the following technical regulations:
1) The concrete chimney must be set up with a lightning needle, the metal chimney must be treated with ground, and the ground resistance should be less than 10Ω;
2) Permanent sampling, monitoring holes and sampling platforms should be set up;
3) The height of the chimney of the heat storage type should not be less than 15m;
4) When there is a building with a radius of 200m around the chimney, the height of the chimney is not less than 3m higher than the height of the building.
17 Set the flatter or the online settlement machine in the continuous annealing unit should have the following functions:
1) Hydraulic pressure and flat rolling system control;
2) Twist of steel straightness adjustment;
3) Extension detection and control;
4) Wit wiping and vacuum device;
5) The wind and dust removal system when the drying is reached;
6) The foggy and purification system when the wet and flat.
18 The cold rolling production crew using steam as a heating medium shall be set up with steam condensation water recycling devices.
19 When the wire rope and the running steel are near the crowded passage, the protective device that prevent steel rope and steel somosoplasty should be set.
20 The main production facilities of cold -rolled projects must be equipped with basic automation and process control level automation systems.
21 The various industrial wastewater generated by the cold rolling production shall be drained according to the characteristics of industrial wastewater. The special sewage of the industrial wastewater drainage pipe network cannot be discharged directly into the plant area, and it must be processed and then reached into the industrial wastewater pipe network of the plant.
22 Chromium -containing waste liquid treatment The second -level reduction of the hexavalent chromium is not allowed to enter the next processing unit; the second -level restoration of water should not be discharged directly into the acid and alkaline wastewater system.
23 The chromium -containing wastewater adjustment pool must be covered with sealing, and the exhaust gas collection and washing facilities must be set.
24 Chromium sludge, tiny sludge, zinc -containing sludge, and sludge must be recycled.
25 Equipment that cannot be broken in water should be set up to safe water supply systems.
26 The storage area of the corrosive medium must take the collection, storage and exclusion measures, and the storage volume must be greater than the maximum 1 storage tank volume.
27 The power load of the cold -rolled project should be carried out in accordance with the first and secondary loads. The first -level load should be powered by the dual power supply. When a power supply fails, the other power should not be damaged at the same time.
28 In the closed cable channels such as cable tunnels, ditches, shallow grooves, vertical shafts, and mezzanines, the thermal pipeline must not be arranged. Cross -gas pipelines, gas pipelines, combustible liquid pipelines, and corrosive media pipelines are strictly prohibited.
29 Radio -category thick meter and convexity meter must meet the relevant provisions of ionizing radiation protection and radiation sources safety and radiation hygiene protection.
30 Camera and supporting equipment in the hazardous area of the explosion must use explosion -proof products that are compatible with the explosive hazard media.
31 Cold -rolling project should set up an automatic fire alarm system at the following fire hazards:
1) Underground oil depot, underground hydraulic station and lubricant;
2) Underground cable tunnel;
3) Total lower transformers;
4) Electric rooms, transformers, operating rooms, control rooms, computer rooms, cable mezzanines, etc. of each production unit.
32 Cold -Rolling Project near the railway flat intersection should design the corresponding road protection signal according to the Taokou grade level.
33 When the medium transported by the workshop pipeline is toxic, flammable, flammable, and explosive, it is strictly forbidden to cross buildings, structures, process devices, production units and tank areas that are not related to the pipeline.
The layout of the 34 workshop in the workshop shall comply with the following regulations:
1) Class A, B, C, and liquid pipelines and gas pipelines shall not pass through buildings, production devices and tanks without production connections with the pipeline;
2) Class A, B, C, and gas pipelines and gas pipelines shall not be laid in the yard and warehouse area where flammable and explosive items are stored, and the production, storage and loading facilities with strong corrosiveness should be avoided;
3) Overhead power lines are strictly forbidden to cross the explosive gas environment, fire hazard areas, and warehouse areas that store flammable and explosive items.
----------------------------//division line//-------------------- ---------------
Foshan Glimpse Engineering Technology Co., Ltd. (Glimpse Technology for short, its predecessor is Xi'an Weibao Metallurgical Equipment Technology Co., Ltd. established in 2014) is located in Foshan, the main distribution hub of stainless steel in China and Glimpse’s headquarter office is located in Foshan Greenland Financial Complex Building. Glimpse is a high-tech company with a team of top metallurgical experts in China, specializing in development, design, manufacture, installation and commissioning of complete sets of cold rolling equipment and strip processing equipment for stainless steel, carbon steel and non-ferrous metals. Glimpse has a professional team of 40 experts and technicians which including 2 well-known steel rolling expert professors (appointed consultants), 4 well-known foreign steel rolling experts (appointed consultants), 8 professor-level senior engineers, 10 senior engineers, and the rest are master degree holders or experienced technicians with medium-grade or above professional titles. Glimpse masters the core technologies of metallurgical fields: cold rolling, tandem cold rolling, annealing, pickling etc. Glimpse cooperates with world first-class professional companies, university research institutes (such as China North Heavy Industries Group, Sinosteel West Heavy, MCC Shaanxi) Press, China Second Heavy, Xi'an University of Technology, Yanshan University, Germany ABB, Germany Siemens, etc.) for long-term strategic cooperation.
Please feel free to contact us by gavin@glimpsetech.cn. Thank you.
 Global Steel Demand Stabilizes in 2026: What Opportunities Lie Ahead for Used Steel Equipment?
 Leveler and Cut-to-Length Lines Move Toward Higher Precision as High-Strength Steel Processing Drives Upgrades
 Cold Mill Rolls: Technology Upgrades Support Higher Precision and Rolling Performance
 Domestic Hot-Rolled Coil Transactions Maintain Year-on-Year Growth, Showing Resilient Market Demand
 Green Steel Transition Accelerates the Construction of Next-Generation Pickling Lines
 Global Steel Producers Continue Investing in New Cold Rolling Mills
 Global Steel Producers Continue Expanding Cold Rolling Capacity
 Global Skin Pass Mill Market Reaches $513 Million in 2025, Projected to Exceed $623 Million by 2032
 The Critical Role of Skin Pass Mills in Cold Rolled Strip Production
 How Roll Configuration Affects Product Quality in Hot Rolling Mills
 July 2023 chinese steel products import and export express
 2023 China Chinese Iron and steel industrial reform in 2023
 China national steel production in May 2023
 GLIMPSE 4 HIGH COLD ROLLING MILL DATA SHEET
 Application comparison between 6-High mill and 18-High mill on high strength steel
 GLIMPSE HC 6 HIGH COLD ROLLING MILL DATA SHEET
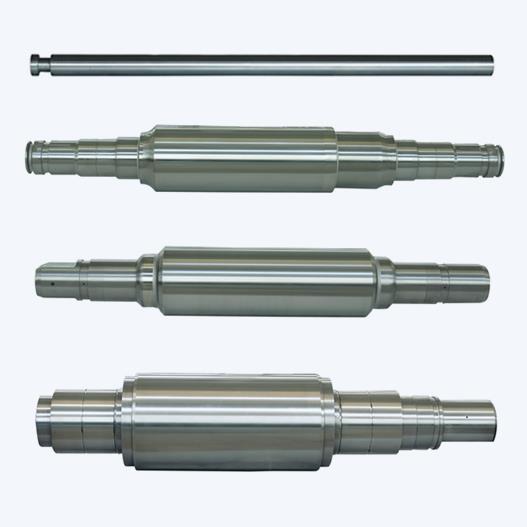 The classification of roll materials
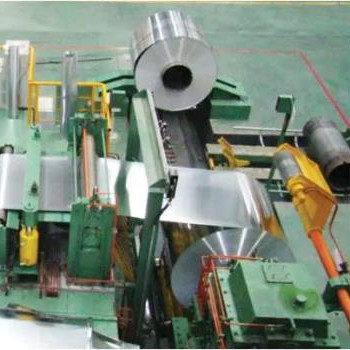 Requirements of cold rolling flat products
 GLIMPSE awarded as a high-quality Chinese supplier of high-quality rolling mill
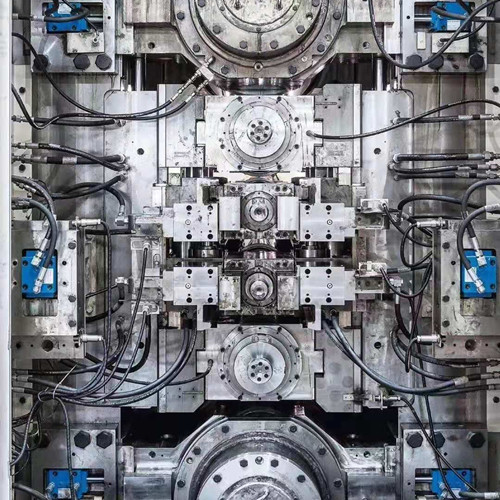 The principle and advantages of CVC rolling mill