
The processing and maintenance of cold roll mills
author: Glimpse
2022-12-02
The processing and maintenance of cold roll mills
Abstract: mill roll is the key contact technology equipment for strip production. In view of the problems in the process of cold rollprocessing, the surface quality is improved in the production process from the aspects of roll grinding, non-destructive testing of rolls, andthe use of rolls, and the production cost is reduced to ensure continuous and efficient operation. Non-destructive testing of rolls is of greatsignificance for the rolling of cold rolled sheets, especially ultrasonic testing. Rolling accidents are reduced during the on-line operation ofthe rolls. According to the attenuation of the roll roughness, the schedule is reasonable, the chrome-plating quality of the chrome-platedrolls and the edge chamfering of the support rolls are optimized to reduce the roll consumption.
0 Preface
With the continuous upgrading of cold rolling products, cold rolling is not only facing ordinary building materials boards, but is moving towards high -end car boards and home appliance boards. The varieties of cold -rolled products have achieved full coverage from low -carbon ultra -low -carbon soft steel series to high -strength and high -strength hard steel series, and the surface quality of the board also needs to further meet the surface requirements of the O5 car. Rolls are directly contacted with steel. The appearance of the surface mill roll surface is equivalent to "mold", which is the key to determining the surface quality of the steel. Higher requirements, higher hardness and higher abrasion resistance on cold rolls or middle mill rolls, and put forward new requirements for metallurgical quality and micro -organizations of the supporting mill rolls, stronger toughness and toughness and toughness and toughness and toughness and micro -organizations. Anti -peeling performance. Improper use of rolls and improper use will cause the roll consumption to rise sharply. This article studies the rolls from the processing, inspection and use of rolls to study the rolls to improve the service life of the rolls, improve the quality of the board, and provide a reference for the quality of the roll consumption of the roll consumption.
1 processing of rolls
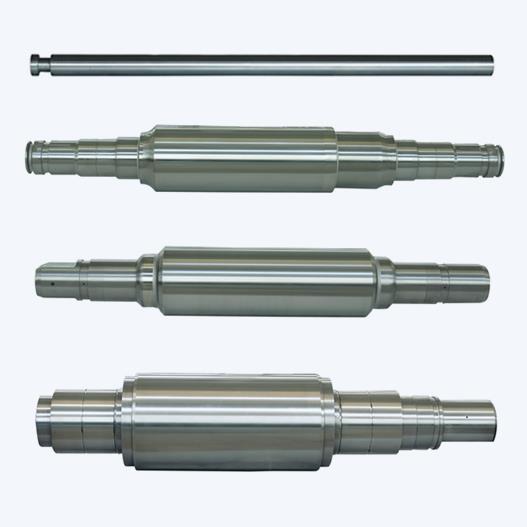
The roll will bear high rolling load during the work, and there are frequent bending, reversing, and mill roll friction. After using a certain period of time , Repair the mill roll curve while gradually removing the fatigue layer. The roll material is a polymer composed of iron-based solid solid solid solution and alloy carbides. The currently adopted CR5 roll with a single grinding amount is 0.2-0.3mm. More than MM.
In addition to the mechanical and equipment factors of the grinding machine, the most critical media and consumables are metal cutting fluids and sand wheels, and the surface quality is improved, which also puts forward higher requirements for metal cutting fluids and sand wheels. Metal cutting fluid requires good dandruff settings, excellent cooling and cleaning, and reducing scratching of mill roll surfaces. Use the appropriate sand wheel model and grinding process parameters to ensure that the mill roll -type problems, surface vibration, horizontal thread wires, and surface pull hair cannot appear during the grinding process.
For hard steel rolls, the Gangyu wheel is generally selected, and the Gangyu sand wheel that matches it according to the material of the roll can achieve high surface quality and grinding accuracy. The problems in the shape of rolls are usually caused by the soft wheel. The surface of the roll on the surface of the roll, the wheel is too hard or the feed rate and the horizontal movement speed are too high. It is necessary to reduce the line speed of the wheel, reduce the amount of sword inlet, reduce the speed of horizontal movement, and increase the roll speed. The horizontal thread wire is also called a knife pattern. When the modifier of the sand wheel is not good or the feed rate, and the horizontal movement speed is too high. When the wheel is too soft, the filtering of the coolant is faulty, the milling particles will cause the grinding point defects on the surface of the roll when floating in the coolant. It is necessary to check the filtering of the coolant, increase the speed of the sand wheel, reduce the roll speed, reduce the amount of sword inlet, Essence The sand wheel is too hard, poor self -sharpness, and the sand particles are not easy to fall off. The grinding mill roll surface is prone to pull -up phenomenon. It is necessary to increase the mill roll speed and reduce the speed of the wheel line.
The grinding of rolls and the cooling properties of the cutting fluid not only affect the surface status of the roll, but also the excessive amount of feed or insufficient cooling will also cause a slight crack on the surface of the roll. Testing such as vortex and ultrasonic detection needs to adjust the sensitivity to high before discovering. The mill roll surface of the grinding burns is tiny crack ultrasonic and magnetic powder detection results. If this grinding slightly crack is not discovered, the use of the machine will cause major accidents and explosive mill rolls.
In order to achieve good deep -rushing and high coating attachment, the surface state is usually anesthesia, and the working mill roll needs to be processed. At present, the hair production method used for high -quality board bands mainly adopts electro -spark hair, and the appearance parameter surface roughness RA, peak density PC value of electro -spark hair can be used. Control of strength, intermittent time, etc. Reduce current or pulse width can reduce the RA value and increase the PC value. The uniformity of capacity and the point -like defects of the hair are related to the quality of carbon powder and electrodes. Unexplained discharge and carbon powder bonding can cause the quality of capacity, leading to repeated grinding and hairy, causing costs to increase. At the same time, watermarks will often occur during the process of capacity. The watermark is bent in waves, and there is a certain color difference on both sides. It is more obvious after chrome plating, which has a serious impact on rolled high -end surface products.
2 Detection of rolls
It is necessary to perform non -destructive detection before the roll is used. Ultrasonic detection, vortex detection, magnetic powder detection and penetration detection are usually used in daily production. The vortex detection has the advantages of fast detection speed, and can detect soft dots defects, but it can only be targeted at the surface flaws and is affected by interference. Excessive sensitivity can easily cause messy signals. The penetration test is only obvious when dealing with the large -scale opening defects of the bureau. The use of ultrasonic powder with magnetic powder detection is more significant for ensuring the normal use of rolls.
The most convenient method of ultrasonic surface wave is to use the bottom wave method, that is, place the probe at the middle 1000mm of the roll body, adjust the water chestnut reflected wave at the end of the roll body to a height of 20%, and then gain 32dB. When the roll is in good condition, the surface of the roll body will not cause abnormal wave reflection regardless of the circumferential and axial detection. However, due to the restriction of the smelting process, there are sometimes tiny pores and loose defects in the outer ring of the roll body. After forging The slender strips are called hairlines, which are randomly distributed along the length direction of the roll body, and the length is mostly 0.05-3mm, which causes abnormal reflection of surface wave detection.
These tiny hair patterns generally have a length of less than 1mm, and it does not affect the quality of the product during use, but it is difficult to distinguish the small cracks produced by rolling rolling rolling rolling during ultrasonic detection. In this case, it is necessary to use magnetic powder detection and micro -observation. The state of the flaws is generally flat for roll manufacturing. The sharp corners are generally crack defects caused by rolling use. The surface crack defect will cause the mill roll surface to peel off, effectively detect the remaining residual cracks of the mill roll surface, and avoid the rolls from being wounded and running. The magnetic powder and ultrasonic detection results of the hair pattern and the enlarged image of residual cracks.
The sensitivity of direct ultrasonic flaw detection is determined by the AVG method to determine the equivalent diameter of the defect, and 20% of the height of the first bottom wave reflection that is less than full screen is taken as the reference height, and then the sensitivity increment of the flaw detection part is calculated according to the following formula to adjust the gain.
Calculate formula n = 20lg (λD/2π),
n ——— The value of sensitivity increase (DB);
D — the thickness of the workpiece (unit mm);
λ — when F = 2.5MHz, the wavelength of ultrasonic waves in the steel (generally take λ = 2.36mm).
After the defect signal is found, use the gain of the instrument to divide the thickness of the detected workpiece into ten equal parts based on the principle of 12, 7, 5, 4, 3, 3, 2, 2, 2. Decrease the corresponding gain value according to the defect position, and use this As a reference, raise or lower the height of this defect wave to 20% of the full scale of the screen.
Generally, the outer layer of the mill roll body of the working mill roll and the middle mill roll is 90mm depth of 90mm. There is no defect back wave, and there is no defect in the middle area that exceeds φ2 15dB. Abnormal wave defects in the center of the work mill roll, although a certain bottom wave has decreased, the assessment of its results is not supermark. The abnormal wave comes from the superposition of the central loose, and the mill roll has not been used to use it.
The use of the support mill roll is 5-10mm depth during the use of the support mill roll.
After offline, it is difficult to find the defects of the deep area after the ultrasonic surface wave detection. The position of its defect formation is relatively shallow with direct probe. When a certain scale is not formed, the detection difficulty will be greater. In this case, improve the sensitivity of the surface wave, screen the grass -shaped waves, and the cluster of the beam position of the cluster focuses on direct detection of ultrasonic detection. Ultrasonic detection and internal and external conditions occur under the roll skin. In subsequent use, the roll is needed to increase the detection tracking, prevent the crack from continuously expanding and causing the entire roll to be scrapped.
3 Roll use
In the case of acid rolling, the hardness of the mill roll of the rolling rolling mill roll requires absolute guarantee, otherwise it will cause the product thickness fluctuations and poor plate shape. The pursuit of mill roll height and hardness will lead to poor mill roll resistance accident capabilities, which puts higher requirements for low production line operation accident rates. A more serious break accident will directly cause a work mill roll worth 100,000 yuan. Automotive appliances and other downstream users put forward higher requirements for cold -rolled products. At the same time, the scope of the surface roughness requirements of automotive steel is narrow. To obtain the surface roughness and surface quality that meets the requirements of the user, it is necessary to reasonably discharge the production plan according to the decay of roll roughness, and extend the cycle of the roll as long as possible to reduce the frequency of the mill roll. Reduce roll consumption.
The mill roll dialing cycle of the support mill roll is relatively small with the structure and specifications of the product. In addition to the internal damage caused by the accident, the roll abnormal consumption is the most stressful position in the mill roll shoulder backward angle of the mill roll. When the corner of the mill roll end is straight, it is easy to form a small and slight cracks. -3mm, grinding removal caused a large roll consumption. If it is not treated in time in subsequent use, it will cause the mill roll to peel off the side of the mill roll. Steering with an arc chamne can effectively reduce the stress concentration of the location. Quality problems such as rolls themselves also cause the anti -fatigue performance of the chamfering parts. Even if optimized the chamfering curve, the mixed defects of the area will cause cracks and expansion, affecting the cycle of the roll.
During the rolling process, chrome -plated mill rolls can reduce the friction coefficient. The amount of iron powder generated during the mill roll seam friction is reduced, which greatly improves the cleanliness of steel after rolling. Increase the average reflectivity of the surface of the board. The pressure of continuous continuous annealing and galvanized cleaning section is reduced, which is conducive to improving the quality of the surface. Table 1 is the effect of using chrome -plated mill rolls in Tanggang Cold Rolling Factory. However, the quality of the coating is very high, and it is necessary to ensure that it cannot fall off under large rolling load. Once the coating falls off, it directly causes the surface defects of the product. The thickness of the normal chrome layer is about 6 μm, and the micro -structure is webly.
4 Conclusion
① The manufacturing control of the roll itself and the optimization of subsequent grinding and texturing processing parameters are the key to ensuring the quality of the roll surface. The first pass rate of roll grinding is increased by 5%, and the overall service life of the roll is extended by more than 2.5%. Lifting and cost reduction play an important role.
② The defect prevention of non-destructive detection, the online detection equipment is running steadily, which basically avoids the losses of rolls from 1-2 per year.
③The attenuation law of the roughness of the roll texture, the quality of the chrome plating of the roll and the design of the operating cycle can increase the output of products that require a high-quality surface by 80%, and basically reduce the single-roll scheduling by 3-5 rolls in each roll cycle It is an important factor to improve product quality and reduce cost.
Keywords: work roll, cold mill roll,cold rolling
 Global Steel Demand Stabilizes in 2026: What Opportunities Lie Ahead for Used Steel Equipment?
 Leveler and Cut-to-Length Lines Move Toward Higher Precision as High-Strength Steel Processing Drives Upgrades
 Cold Mill Rolls: Technology Upgrades Support Higher Precision and Rolling Performance
 Domestic Hot-Rolled Coil Transactions Maintain Year-on-Year Growth, Showing Resilient Market Demand
 Green Steel Transition Accelerates the Construction of Next-Generation Pickling Lines
 Global Steel Producers Continue Investing in New Cold Rolling Mills
 Global Steel Producers Continue Expanding Cold Rolling Capacity
 Global Skin Pass Mill Market Reaches $513 Million in 2025, Projected to Exceed $623 Million by 2032
 The Critical Role of Skin Pass Mills in Cold Rolled Strip Production
 How Roll Configuration Affects Product Quality in Hot Rolling Mills
 July 2023 chinese steel products import and export express
 2023 China Chinese Iron and steel industrial reform in 2023
 China national steel production in May 2023
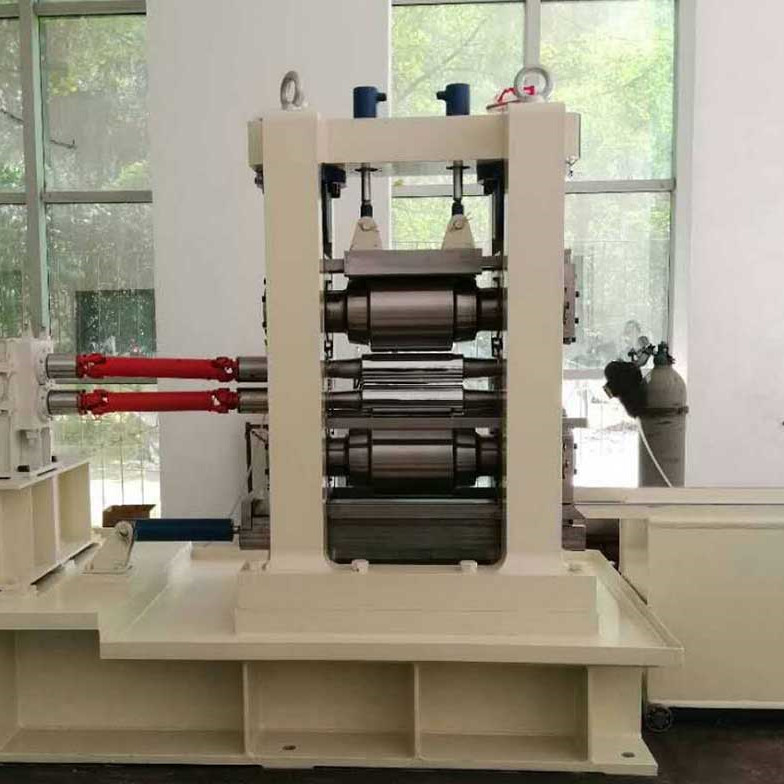 GLIMPSE 4 HIGH COLD ROLLING MILL DATA SHEET
 Application comparison between 6-High mill and 18-High mill on high strength steel
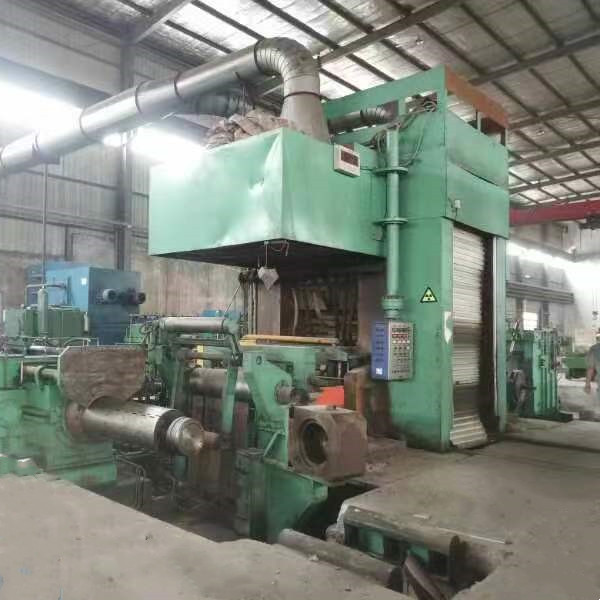 GLIMPSE HC 6 HIGH COLD ROLLING MILL DATA SHEET
 The classification of roll materials
 Requirements of cold rolling flat products
 GLIMPSE awarded as a high-quality Chinese supplier of high-quality rolling mill
 The principle and advantages of CVC rolling mill