
What Is Roll Separating Force (R.S.F.)
What Is Roll Separating Force (R.S.F.)
In metalworking, rolling is a metal forming process in which metal stock is passed through one or more pairs of rolls to reduce the thickness, to make the thickness uniform, and/or to impart a desired mechanical property. The concept is similar to the rolling of dough. Rolling is classified according to the temperature of the metal rolled. If the temperature of the metal is above its recrystallization temperature, then the process is known as hot rolling. If the temperature of the metal is below its recrystallization temperature, the process is known as cold rolling. In terms of usage, hot rolling processes more tonnage than any other manufacturing process, and cold rolling processes the most tonnage out of all cold working processes.
The basis of understanding rolling is knowing the forces created by rolling, the main one being Roll Separating Force(R.S.F.). During rolling, the strip is deformed, but so is the mill housing. The difference is that the deformation of the strip is permanent (plastic) while the deformation of the mill is temporary (elastic).
It is not possible to understand rolling if the notion of deformation is ignored.
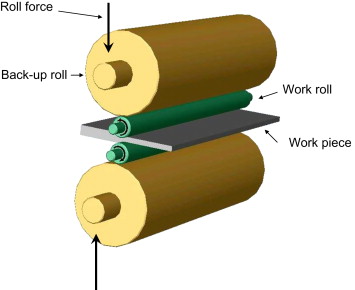
During rolling process, the strip acts as a wedge between the two rolls and creates the forces F and F (figure 1.1). This is the R.S.F.

All parts of the housing experience R.S.F.
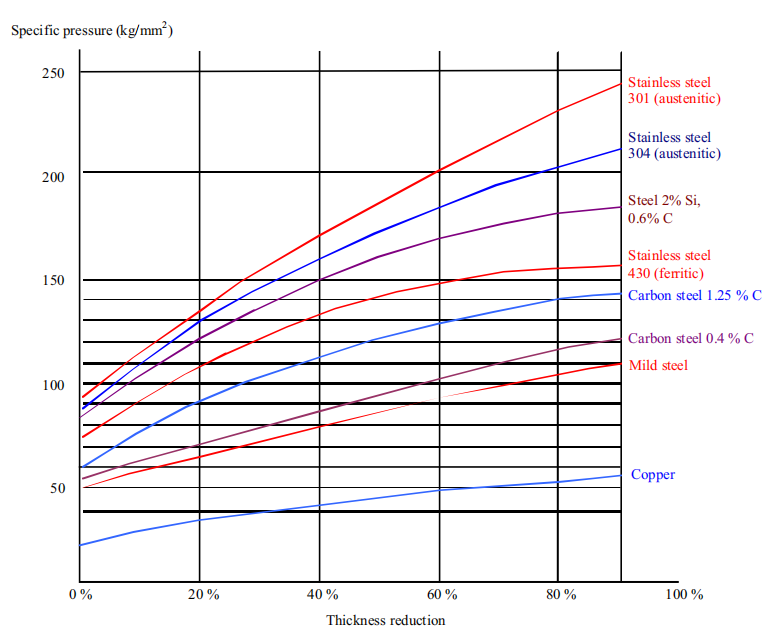
For a given mill, the higher the reduction and the harder the material, the higher the R.S.F.
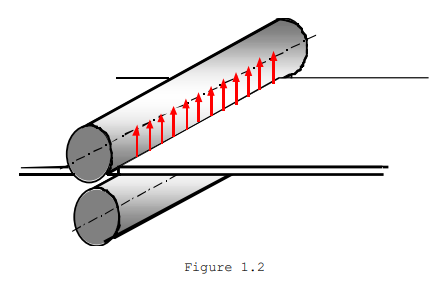
The R.S.F. is uniformly distributed along the width of the strip (figure 1.2) and is proportional to the strip width.
The consequences of R.S.F. are:
• roll bending (figure 1.3),
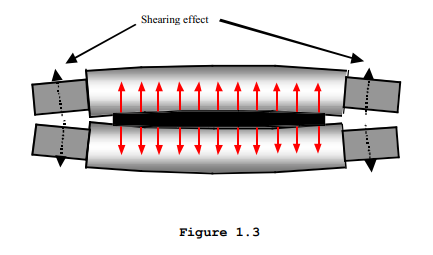
• a shearing effect on the necks of the rolls (figure 1.3), Shearing effect Figure 1.3
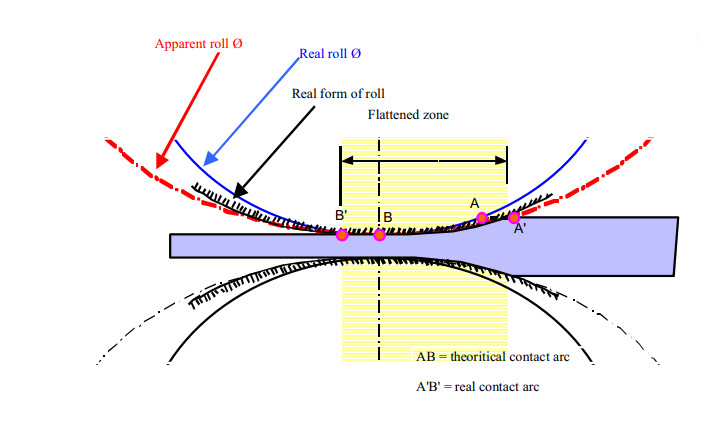
• roll flattening: the rolls are flattened where they make contact with the strip as well as with any other roll,
• deformation of the housing: some parts are in compression, others in tension,
• an axial force on the rolls, if the strip is thicker on one side than on the other (figure 1.4).
Rolling force is an important factor in mill design. In the design stage, it is very important to determine how much rolling force is required according to the mechanical properties of materials, roll diameter and other parameters.
 Why choose AC motor for cold rolling? (I) Disadvantages of DC Motor
 Steel strip rolling process – roll separating force
 Cold rolling mill maintenance and safety technology
 What is the training program about under a sales contract of 20 high cold rolling mill?
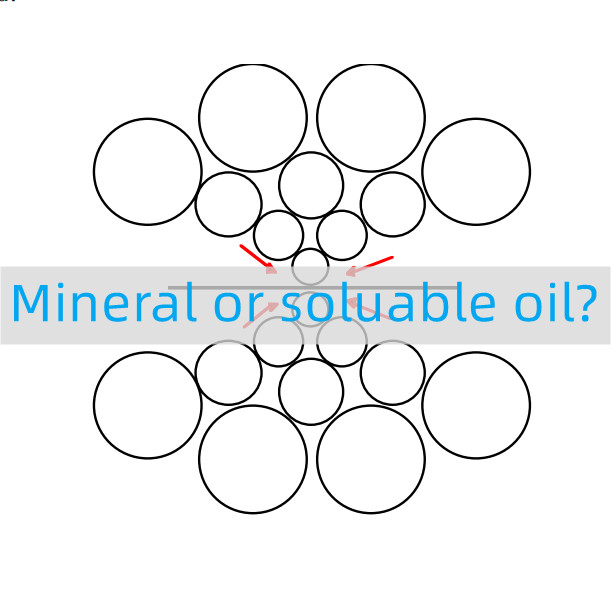 Which is better? Soluble or mineral oil?
 Q8 Roll hardness check
 Q 7 How to properly do roll grinding check?
 Viscosity Classification Equivalents
 Q6: How to do roll storage inspection
 Q 5: What is roll service cycle?
 Q 2 What to do during roll incoming inspection?
 Q1 How to select a supplier of mill rolls?
 The training program for operators of cold rolling mills
 The General principle of rolling speed regulation for cold rolling mills
 Why are stainless steels hard to roll?
 How to choose competent operators for cold rolling mills
 A brief introduction of 20 high cold rolling mill
 Pass schedules for reversible cold rolling mills.
 The design of work roll diameter
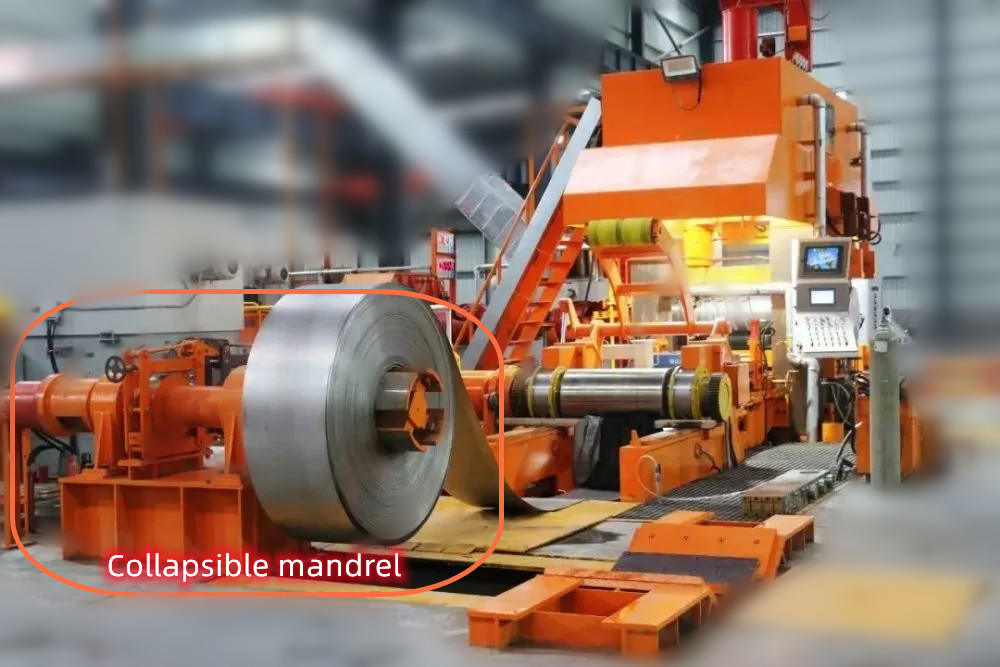 Types of coilers in metal rolling operation